Direct Answer: How Gummies Are Made at Commercial Scale
To make gummies at commercial scale, you need to move from a kitchen recipe to a controlled manufacturing process: validated formulation, precise thermal processing, timed addition of heat-sensitive actives, automated depositing, controlled drying to target water activity, and barrier packaging with full QC release. Working with an experienced gummies manufacturer early reduces scale-up risk, because dosage, gel structure, and moisture control are locked before you invest in tooling and production.
In gummy manufacturing, the sequence matters. The gel system is cooked to achieve target solids and texture, pH and flavor systems are balanced, active ingredients are added at the lowest viable temperature, the mass is deposited into molds, cooled to set, dried or conditioned to a stable water activity, then inspected, counted, and packed. Each stage has measurable parameters that affect texture, potency retention, and shelf life. The sections below cover formulation decisions, the eight production steps, in-process quality controls, cost drivers and MOQ, and how to evaluate a manufacturing partner.
Overview
Commercial-scale gummy production requires tight control over formulation, cooking, molding, drying, coating, and packaging, all carried out under GMP-certified conditions. For brand owners and distributors, understanding this process is essential for evaluating production partners, planning production timelines, and ensuring consistent product quality. This guide explains how gummies are produced at commercial scale, the technical parameters that determine success, and the factors B2B buyers should assess before sourcing.
Definition
Commercial production of gummies refers to the industrial process of turning a gummy formulation into a finished, packaged product through standardized stages—ingredient preparation, cooking, depositing, molding, drying, coating, and packaging—typically carried out in GMP-compliant facilities with quality-control checkpoints at each stage.
Why Commercial Gummy Manufacturing Is Different From Kitchen-Scale Production
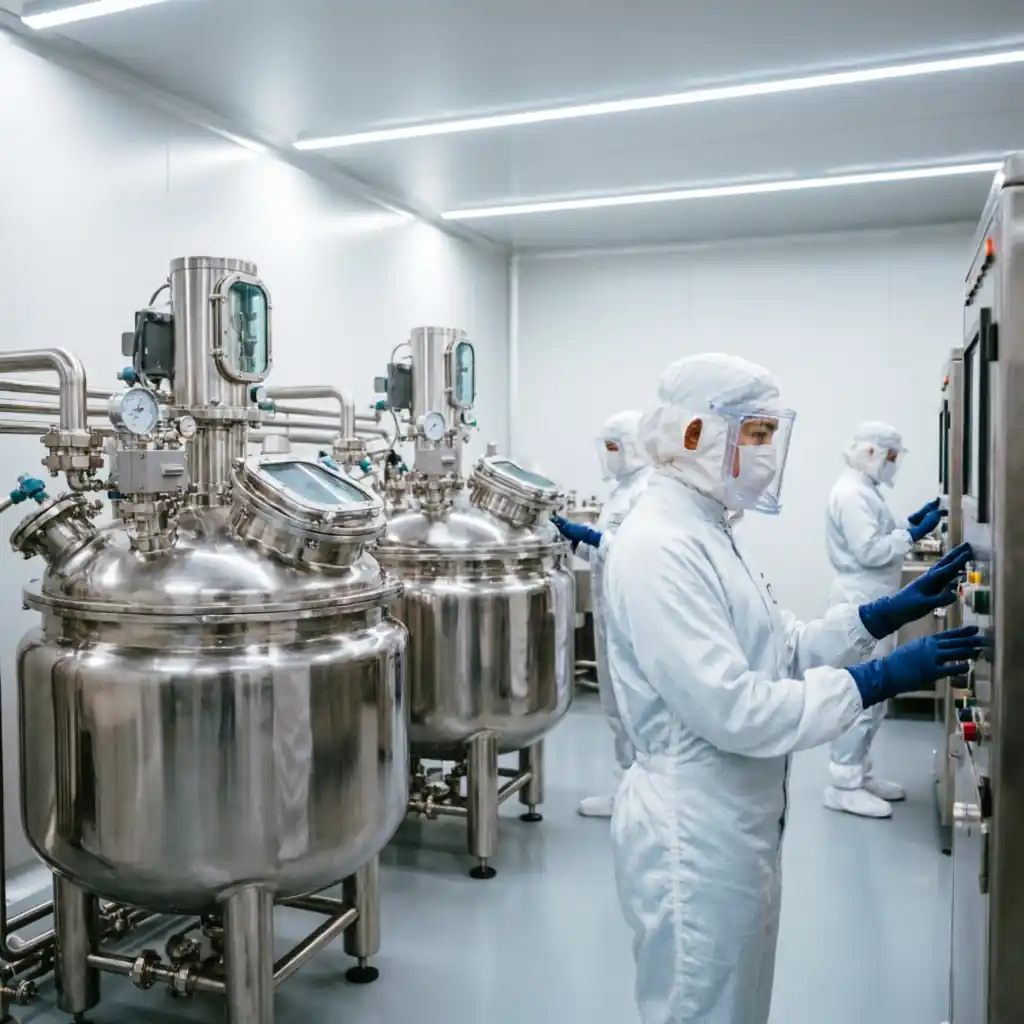
Kitchen batches tolerate variation. Commercial batches do not. At 100 kg to over 1,000 kg per lot, small errors in temperature, pH, or depositing time create thousands of out-of-spec units.
Four differences drive most sourcing failures. First, heat exposure time is longer at scale, which accelerates degradation of vitamins, probiotics, and botanicals. Second, water activity must be controlled to below 0.75 for most supplement gummies to limit microbial growth and stickiness. Third, texture must be consistent across the entire cooling tunnel, not just the center tray. Fourth, active distribution must be uniform so each gummy meets label claim within USP or target market tolerances.
Key Takeaways
What Does Commercial-Scale Gummy Manufacturing Involve?
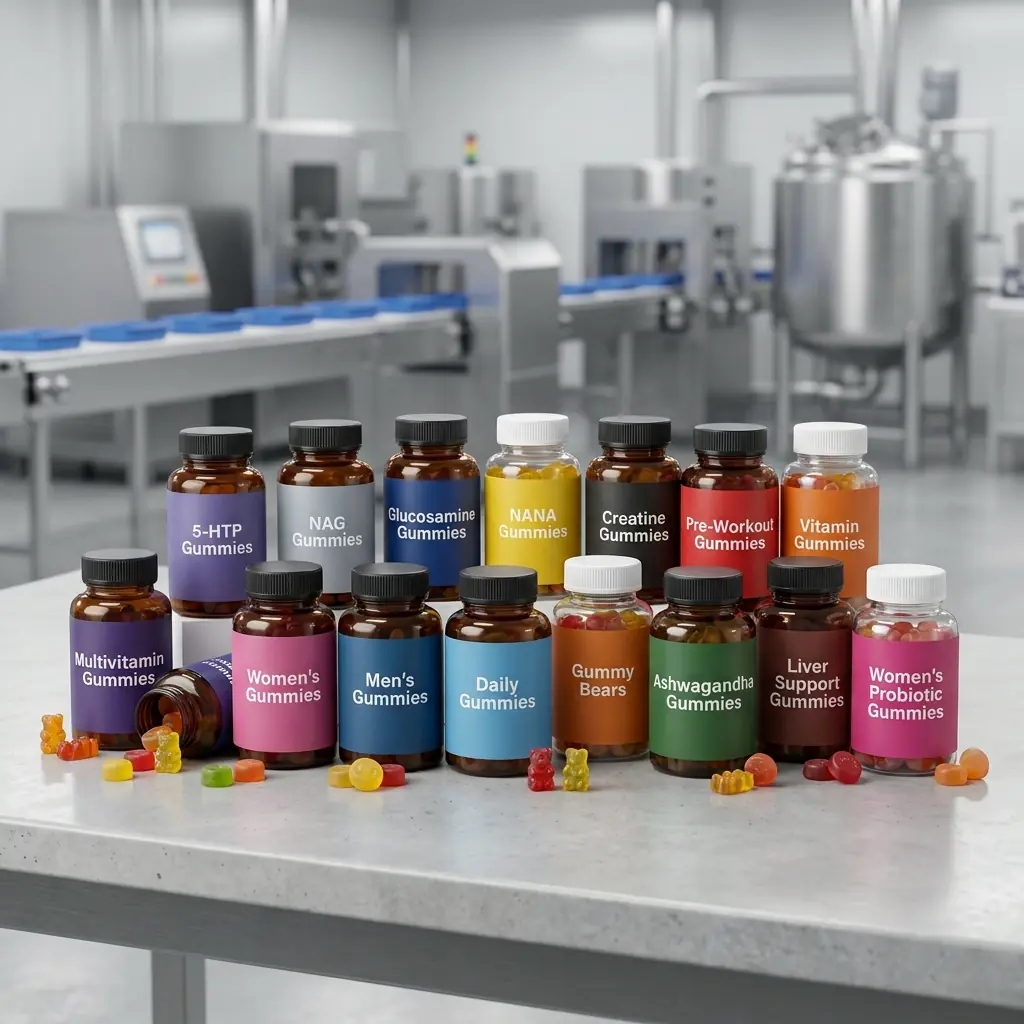
Commercial gummy production goes far beyond small-batch or cottage-style methods. It demands precise formulation control, industrial cooking equipment, automated depositing and molding systems, and standardized drying and coating processes, all designed to produce thousands of units with consistent shape, texture, and potency. With the right equipment and quality-control system, a contract manufacturer can deliver gummies that match specifications exactly from batch to batch.
Industry Context
Gummy supplements have evolved from a novelty product into one of the fastest-growing categories in the dietary supplement industry, driven largely by consumer preference for great-tasting, easy-to-take formats. This growth has pushed manufacturers to scale output while maintaining dosage precision and quality standards comparable to pharmaceuticals.
Commercial Relevance
For brands entering or expanding their gummy range, production scale directly affects unit cost, lead times, and speed to market. Supply-chain factors—including raw material sourcing, equipment capacity, and packaging-line flexibility—determine whether a manufacturer can handle both trial orders and high-volume orders at the same time.
Core Production Stages
- Formulation development: Selecting gelling agents (pectin, gelatin, or carrageenan), sweeteners, active ingredients, flavors, and colors, then testing for stability and taste.
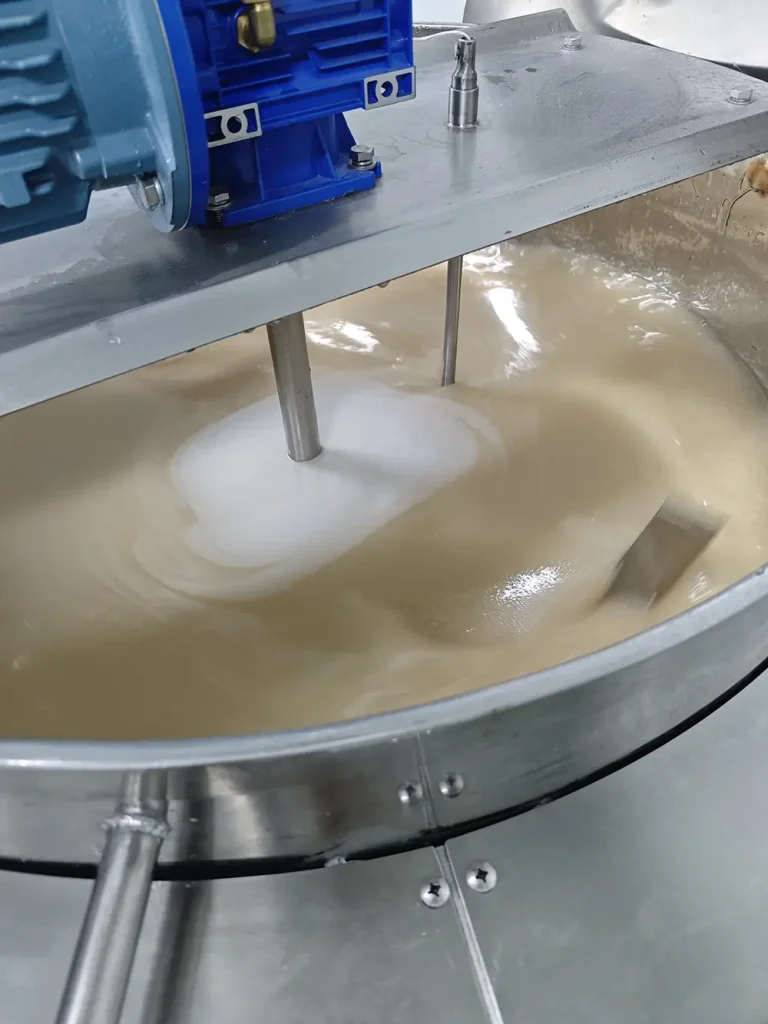
- Cooking and mixing: Combining ingredients under controlled temperature and time to reach the correct viscosity and solubility.
- Depositing and molding: Filling the gel mixture into molds using starch or silicone mold systems to create consistent shapes.
- Drying and setting: Reducing moisture content to reach the target texture and shelf stability, typically requiring 24–72 hours.
- Coating: Applying an oil or sugar coating to prevent sticking and improve mouthfeel.
- Packaging: Filling into bottles, pouches, or blister packs and labeling in line with the regulatory requirements of the destination market.
Differences and Alternative Formats
Compared with capsules, tablets, or powders, gummies require extra processing steps to control texture and shape, longer drying cycles, and stricter humidity control in storage. This makes gummy production more demanding in terms of equipment and time, but the format is more appealing on retail shelves and easier to differentiate.
Key Advantages and Limitations
Advantages include higher consumer acceptance, flexibility in flavor and shape design, and stronger shelf appeal. Limitations include greater sensitivity to temperature and humidity during production and storage, typically lower active-ingredient loads than tablets or capsules, and longer production cycles caused by drying requirements.
Who Should Consider Commercial Gummy Manufacturing
This process is especially relevant for wellness brands launching new product lines, distributors seeking private-label options, and OEM/ODM buyers in need of a custom gummy manufacturer. The right manufacturer can scale from pilot batches to full commercial production without compromising consistency.
Compliance and Quality Considerations
Commercial gummy production should take place in facilities certified to GMP, ISO 9001, ISO 22000, and HACCP, with documented quality control at every production stage. For export production, third-party testing for potency, microbiological safety, and heavy metals is standard practice.
What Factors Should Businesses Evaluate Before Sourcing
Before selecting a production partner, buyers should evaluate production capacity, minimum order quantities, formulation flexibility, the certification portfolio, and the manufacturer’s ability to provide documentation supporting regulatory compliance in the target market.
Core Formulation Decisions Before You Make Gummies
Gel System Selection: Gelatin vs Pectin vs Hybrid
Gel choice determines process, texture, claims, and stability. Gelatin gives elastic chew, lower depositing temperature (typically 80–90°C), and good clarity, but it is not vegan and can melt at high ambient temperatures. Pectin gives a short, tender bite, heat stability, and vegan positioning, but requires tight pH control (3.2–3.8 for high-methoxyl pectin) and higher depositing temperatures (90–105°C).
For a B2B buyer, the decision affects more than claims. Gelatin systems are more forgiving on acid and flavor oils. Pectin systems are more sensitive to calcium, acid addition timing, and soluble solids (usually 76–80 Brix). Hybrid starch-pectin or pectin-gelatin systems are sometimes used to balance texture and process window.
| Attribute | Gelatin Gummy | Pectin Gummy (High-Methoxyl) |
| Typical Texture | Elastic, chewy, bounce | Short, soft, less chewy |
| Vegan Claim | No | Yes |
| pH Sensitivity | Moderate, degrades below pH 3.5 | High, requires precise acid addition |
| Depositing Temp | 80–90°C | 90–105°C |
| Heat Stability of Finished Gummy | Lower, risk of melting in transit | Higher, better for warm markets |
Active Ingredient Loading and Gummy Weight
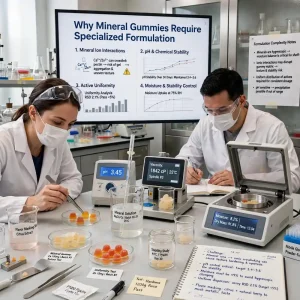
Active loading drives gummy size and serving count. High-dose ingredients like magnesium citrate, calcium carbonate, or fiber increase solids and can make gummies grainy or too large. Most commercial supplement gummies are 2.5 g to 4.0 g per piece.
If dosage exceeds 300–400 mg of bulky minerals per serving, you will either need a larger gummy, a higher serving count, or a different delivery format. For potent actives like vitamin D3, zinc, or melatonin, overage strategy and uniform dispersion matter more than size.
pH, Water Activity, and Heat Sensitivity
pH affects gel strength, flavor, and active stability. Vitamin C and sodium citrate buffers lower pH and can weaken gelatin. Calcium salts can pre-gel pectin if added too early. Final pH is usually targeted at 3.0–4.0 for flavor and preservation, but must be validated against gel performance.
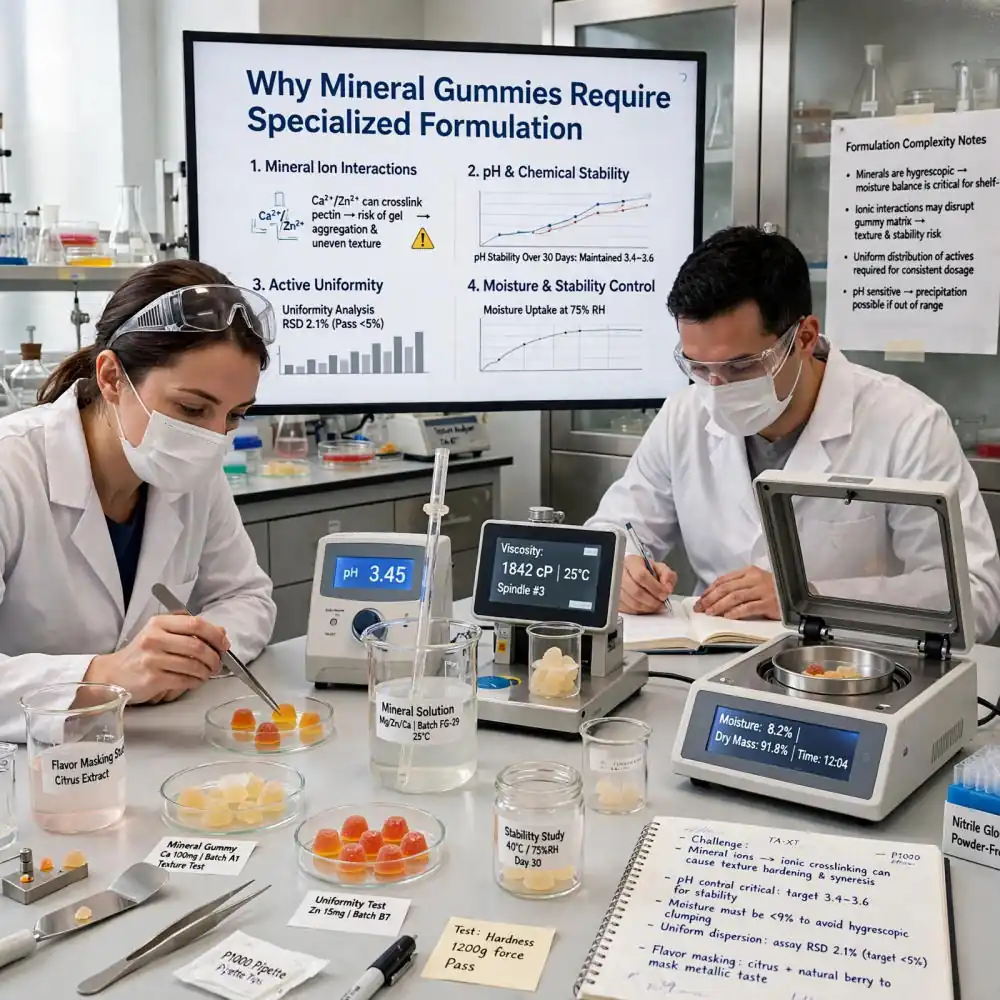
Water activity (Aw) is the primary control for microbial stability and texture over shelf life. Target Aw of 0.65–0.75 after drying reduces stickiness and limits mold and yeast risk. Hygroscopic ingredients like magnesium, potassium chloride, and certain botanical extracts pull moisture back into the gummy after drying and require conditioning studies.
Heat-sensitive ingredients including probiotics, vitamin C, B vitamins, enzymes, and many botanicals should not go through the main cooking step. In commercial practice, they are added as a pre-mixed slurry after cooking, just before depositing, with jacketed holding tanks kept below degradation thresholds.
Step-by-Step Gummy Manufacturing Process
1. Specification Review and Formula Development
Manufacturing starts with a specification review: target actives per serving, gummy weight, gel system, sugar vs sugar-free, flavor, color source, claims, and market. R&D checks ingredient compatibility, regulatory status in target markets, and whether dosage fits the gel matrix without compromising texture.
2. Raw Material Testing and Pre-Batching
Incoming raw materials are tested for identity, potency, and microbiology. Gelatin bloom strength, pectin grade, sweetener Brix, and active assay are confirmed. Color and flavor are matched to standards because natural colors shift with pH and heat.
3. Cooking and Solids Control
Sugars, glucose syrup or sugar alternatives, water, and gelling agent are cooked to target soluble solids. For pectin, solids of 77–80 Brix are typical; for gelatin, 75–78 Brix. Temperature control is critical because it sets final moisture and texture. Overcooking increases browning and hardens texture; undercooking leaves excess water that raises Aw.
4. Active Ingredient Addition and Mixing
The cooked mass is cooled in a holding tank to a defined addition window. pH adjusters, active premixes, flavor, color, and acid are added under controlled agitation. Mixing time is short but must be enough for homogeneity without incorporating air that creates bubbles and weight variation.
5. Depositing and Molding
Automated depositors dose precise mass into silicone or metal molds on trays. Depositor accuracy is typically +/- 1–2% by weight at scale. Vacuum and anti-foaming control improve weight uniformity. Mold design affects demolding and brand differentiation, but custom molds increase lead time and cost.
6. Cooling, Setting, and Drying
Gummies are cooled in tunnels to set the gel network. Pectin gummies set faster via pH and solids; gelatin requires chilled setting. After demolding, most supplement gummies go through drying or conditioning rooms at 20–25°C and controlled humidity for 24–72 hours to reach target Aw and firmness. Skipping or shortening drying is a common cause of clumping in bottles during transit.
7. Coating and Inspection
Optional coating includes oil, wax, or sanding sugar to reduce sticking. Probiotic gummies often use oil-based coating to limit moisture uptake. After coating, product passes through metal detection, visual inspection, and check-weighers to remove deformed or light pieces.
8. Packaging and Finished-Product Testing
Packaging choice directly affects stability. Bottles with induction seals and desiccant are common for supplement channels. Stand-up pouches with high-barrier film lower shipping weight but need heat-seal validation. Finished-product testing includes active assay by HPLC or other validated methods, Aw, pH, texture profile when needed, microbiology (TAMC, TYMC, E. coli, Salmonella), and organoleptic evaluation.
Critical Quality Controls in Gummy Manufacturing
Batch consistency depends on in-process controls, not just finished-product testing. Commercial lines monitor Brix in cooking, pH before and after acid addition, depositing temperature, gummy weight every 15–30 minutes, and Aw after drying.
Microbiological risk in gummies comes from high moisture and sugar handling. GMP controls include water quality testing, environmental monitoring in depositing and packing rooms, allergen cleaning validation when gelatin and vegan lines share space, and validated sanitation of molds and trays.
Shelf-life validation should cover active stability, texture, color fading, flavor change, and Aw drift under ICH or brand-defined conditions. Natural colors like anthocyanin and curcumin are especially prone to pH and light-related fading.
Common Technical Challenges When You Make Gummies
Some concepts fail not because the formula is wrong, but because the ingredient combination is not compatible with a gummy matrix at scale.
- High mineral load: Calcium and magnesium salts create salty, bitter notes and interfere with gelation. Flavor masking and buffered salts are required, and serving size may need to increase.
- Acidic actives: Vitamin C, citric acid-based flavors, and some fruit extracts lower pH enough to hydrolyze gelatin or cause syneresis in pectin.
- Hygroscopic ingredients: Choline, some amino acids, and honey solids attract moisture after drying and lead to sticky gummies in bottles.
- Botanical extracts: Extracts bring color variation, ethanol residues, and bitter notes. Standardized extract grade and de-flavored versions matter for batch consistency.
- Probiotics and enzymes: Require low-temperature processing, low Aw, and moisture-barrier packaging. Survival claims need stability data, not just input count.
Technical Specifications Table
| Scope | Details |
|---|---|
| Product form | Gummies (pectin-based, gelatin-based, or carrageenan-based) |
| Key materials / ingredients | Gelling agents, sweeteners, active ingredients, natural flavors and colors |
| Typical gummy weight | 2.5–4.0 g per piece for most commercial supplement gummies |
| Process control targets | Final pH 3.0–4.0; finished Aw 0.65–0.75; cook solids 75–80 Brix |
| Manufacturing process highlights | Specification review, cooking, depositing, molding, drying, coating, packaging |
| Quality standards | GMP, ISO 9001, ISO 22000, HACCP, third-party testing |
| Packaging options | Bottles, stand-up pouches, blister packs, sachets |
| Scalability and production capacity | From pilot runs to large-scale commercial production; typical minimum 100,000–300,000 gummies per SKU |
| Storage and logistics considerations | Temperature- and humidity-controlled warehousing; moisture-proof packaging for export shipping |
Cost Drivers and MOQ in Commercial Gummy Production
Gummy cost is not driven by gel alone. Active ingredient cost, overage, gummy weight, flavor system, color source, and packaging dominate. Natural flavors and colors cost more than artificial and vary by season.
| Cost Factor | Why It Matters | What to Specify to Control Cost |
| Active dosage and overage | Higher potency or unstable vitamins require more input to meet label at expiry | Target market shelf life, stability requirements, assay tolerance |
| Gummy weight and count per bottle | Weight sets raw material use and bottles per batch yield | Fix gummy weight early, e.g. 3.0 g, and serving count |
| Gel system and sweetener | Pectin and sugar-free polyols cost more than gelatin and sugar | Decide vegan, sugar-free, and sugar alcohol tolerance early |
| Flavor and color | Natural systems need masking and are less stable | Provide target flavor profile and natural vs artificial preference |
| Mold and packaging | Custom molds and specialty bottles increase tooling and MOQ | Use stock molds and standard bottles for first run if speed matters |
| Testing and documentation | Full panel testing, allergen, heavy metals, and export docs add cost | Align testing with destination market requirements |
MOQ becomes commercially important when custom molds, sugar-free bases, or low-volume botanicals are involved. Most commercial gummy lines have a minimum batch size tied to cooker and depositor volume, often 100,000 to 300,000 gummies per SKU. If your first order is below that, ask whether pilot batches, flavor variations from a common base, or shared production scheduling are available.
How to Evaluate a Gummies Manufacturer for Commercial Production
A qualified gummies manufacturer should be evaluated on verifiable capabilities, not marketing claims. Focus on systems that directly affect your product type.
- GMP and quality systems: Look for GMP-certified manufacturing, ISO 22000, HACCP, and documented batch records and traceability. Certifications such as ISO 9001, BRC, FSSC 22000, HALAL, KOSHER, and Vegan indicate system maturity but do not replace market-specific product compliance.
- R&D and pilot-to-commercial scale-up: Ask whether the manufacturer has a 10,000-class R&D lab, texture and Aw testing, and pilot equipment that mimics commercial cooking and depositing. Formulation that works at bench scale can fail at commercial shear and cooling rates.
- Equipment and capacity: Confirm daily and annual capacity, number of depositing lines, cooling tunnels, and drying rooms. A facility with approximately 16 tons daily and 5,000 tons annual capacity provides flexibility for scaling, but ask about current line loading and lead times.
- Ingredient sourcing and compatibility experience: Ask for examples of similar active loading, e.g., high-dose vitamin C, zinc plus elderberry, or creatine gummies, and how they solved taste or stability issues.
- Testing and documentation: Verify in-house and third-party testing for potency, Aw, and microbiology, plus COA, allergen statements, and manufacturing documentation needed for your market.
- Packaging capability and export experience: Check whether the manufacturer can do bottle counting, induction sealing, pouch filling, and labeling in-house, and whether it has export experience with your destination country.
- Commercial terms and formulation ownership: Define scope, formulation ownership, and agreed quality specifications in writing before custom development. Transparent pricing and responsive technical support matter as much as the initial quotation for repeat orders.
- Verification before commitment: Request facility audits, pilot sample batches, and references from existing clients, and set QA checkpoints at raw material intake, in-process production, and pre-shipment stages.
Shenzhen Gothink Biotech Co., Ltd. operates as a China-based dietary supplement manufacturer providing OEM, ODM, CMO, and CDMO services across gummy, capsule, tablet, powder, liquid, and drop formats. Its GMP-certified facility includes a 100,000-class cleanroom and a 10,000-class R&D laboratory supporting custom formulation and scale-up validation.
Common Mistakes Brands Make When Scaling Gummies
- Locking gummy weight and serving count before checking active compatibility. The formula then requires an unacceptably large gummy.
- Adding heat-sensitive actives during cooking instead of after, causing potency loss and failed COA.
- Choosing pectin for cost reasons without accounting for pH control and higher depositing temperature requirements.
- Using natural color without stability testing, leading to faded gummies after 3–6 months.
- Under-drying to save time, resulting in high Aw, clumping, and microbial failures during summer transit.
- Requesting custom molds and complex shapes for the first production, which increases tooling cost and extends timelines.
Practical Checklist Before Requesting an OEM/ODM Quotation
Provide this information to a manufacturer to get an accurate quotation and realistic feasibility feedback:
- Target active ingredients and dosage per serving, and whether dosage is per 1 or 2 gummies
- Preferred gel system and claims: gelatin or pectin, vegan, sugar-free, allergen-free
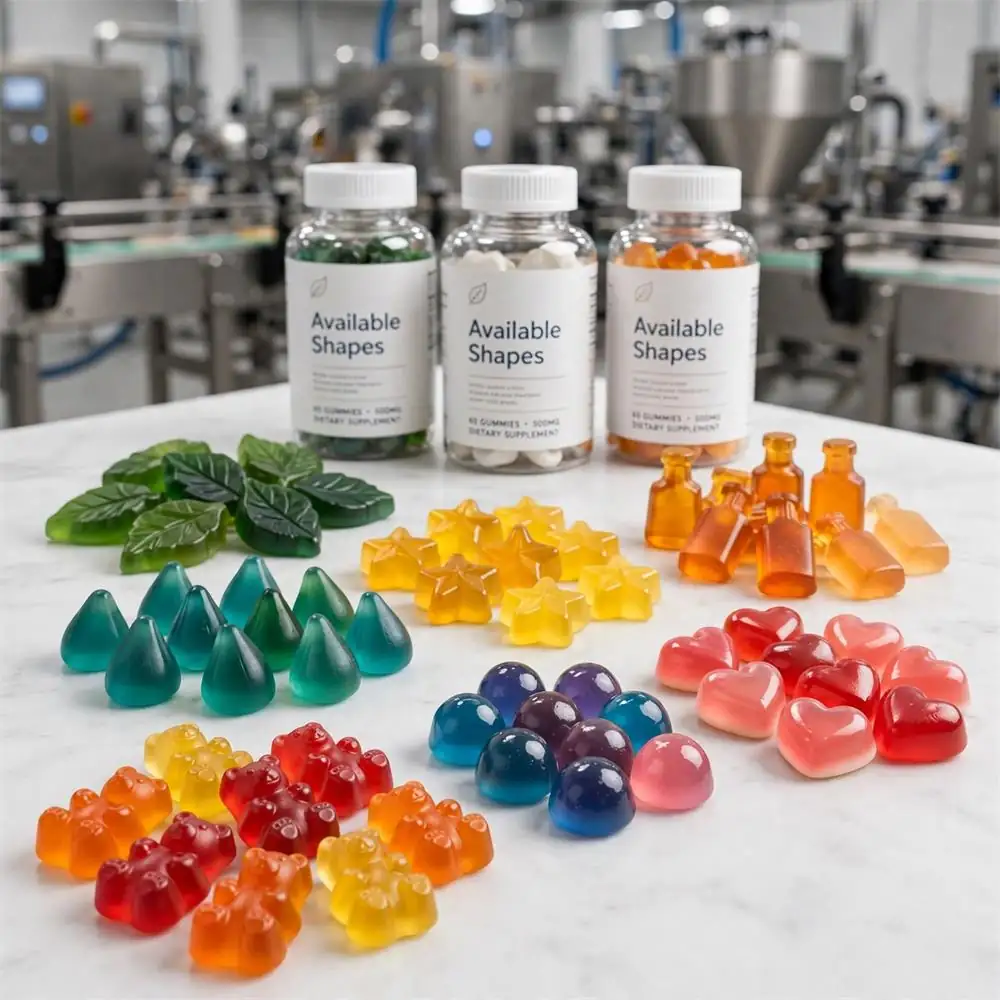
- Gummy weight, shape preference, flavor, and color direction
- Target Aw, texture preference, and any transit conditions (e.g., Middle East summer)
- Packaging format: bottle size, count, pouch, desiccant, label requirements
- Target shelf life and markets for sale
- Estimated annual volume and first-order MOQ flexibility needed
- Testing requirements: potency, microbiology, heavy metals, and documentation
If you are comparing formulation options, ask your manufacturer to show feasibility on a stock mold and standard bottle first. You can review gummy OEM manufacturing capabilities and request a custom formulation development proposal with your spec sheet to shorten development cycles.
Practical Insights
Manufacturing Quality & Process Control: Consistent gummy quality depends on tightly controlled cooking temperatures, accurate depositing volumes, and monitored drying cycles. Manufacturers with automated systems and in-line quality checks reduce batch-to-batch variation.
Raw Material Sourcing Transparency: Reliable suppliers provide certificates of analysis and traceability documentation for gelling agents, actives, and flavoring systems, supporting both quality assurance and regulatory audits.
Production Scalability & Lead Time: Buyers should confirm a manufacturer’s capacity to move from sample development to full production without significant delays, particularly for time-sensitive product launches.
Compliance & Documentation Readiness: Export-ready manufacturers maintain up-to-date certifications and can supply documentation required for customs clearance and market registration in the destination country.
Cost Structure Considerations: Unit costs are influenced by formulation complexity, order volume, packaging choice, and the degree of customization requested.
Evaluating a Reliable Supplier: Look for facility certifications, sample turnaround time, willingness to share process documentation, and a track record of consistent output across multiple order cycles.
Conclusion
Commercial-scale gummy production combines precise formulation science with industrial process control to deliver a consistent, market-ready product. From gel selection and cooking solids to drying, water activity, and barrier packaging, each step has measurable parameters that determine potency, texture, and shelf life. For brand owners and distributors, choosing a production partner with credible certifications, transparent processes, and scalable capacity is key to a successful private-label gummy program. Understanding each production stage helps procurement teams ask the right questions and make informed sourcing decisions.
Frequently Asked Questions
What is commercial-scale gummy production?
It is the industrial process of producing gummies through standardized formulation, cooking, depositing, molding, drying, and packaging steps under GMP quality control, enabling stable production at high volume with consistent shape, texture, and potency.
Why does the production process matter so much to brand owners?
Understanding the process helps brands evaluate manufacturers accurately, forecast lead times, and set realistic expectations for product consistency, potency retention, and cost.
How does gummy production differ from capsule or tablet production?
Compared with capsules or tablets, gummy production requires extra cooking, molding, and drying steps, longer production cycles, tighter pH and water activity control, and moisture-barrier packaging.
What information does a gummies manufacturer need to quote a custom gummy?
A manufacturer needs actives and dosage per serving, gummy weight target, gel system, sweetener system, flavor and color direction, packaging format and count, target shelf life, destination market, and estimated volume. With this, R&D can assess compatibility, size feasibility, and cost drivers before pilot work.
Can all vitamins and minerals be made into gummies?
Not all at commercially viable dosage. Minerals like calcium and magnesium and high-dose fiber are bulky and affect taste and texture. Fat-soluble vitamins need emulsification. Each formula needs a compatibility check for pH, moisture, and heat exposure.
How do you handle heat-sensitive ingredients in gummy manufacturing?
Heat-sensitive ingredients are added after the main cooking step in a temperature-controlled holding tank, usually below 85°C for gelatin systems, with short holding time before depositing. Overage is calculated based on stability data, and Aw and packaging are tightened to protect potency.
What water activity should supplement gummies target?
Most supplement gummies target finished Aw of 0.65–0.75 after drying and conditioning. Lower Aw improves microbial stability and reduces sticking, but very low Aw can make pectin gummies too firm. The target should be validated with texture and stability studies.
What is the typical MOQ for commercial gummy production?
MOQ depends on line size, mold availability, and active cost. Common commercial minimums range from 100,000 to 300,000 gummies per SKU for standard molds and packaging. Custom molds, sugar-free bases, or specialty actives may raise MOQ due to batch size and material ordering.
How long does scale-up from sample to commercial production take?
After formula approval, pilot samples typically take 2–4 weeks, stability bracketing starts in parallel, and first commercial production takes 6–10 weeks depending on raw material lead time, mold tooling, and testing. Export documentation and packaging print can add time.
How should I choose between gelatin and pectin for my market?
Choose gelatin for cost-effective chewy texture and easier processing if a vegan claim is not required. Choose pectin for vegan positioning and better heat stability in warm climates. Your decision should consider the pH of your actives, flavor system, and distribution temperature exposure.
What should a business consider before choosing a gummy manufacturer?
Buyers should assess certifications, production capacity, MOQ flexibility, formulation and R&D support, in-process quality controls, and documentation readiness before selecting a supplier.
What quality standards apply to commercial gummy production?
GMP, ISO 9001, ISO 22000, and HACCP are common quality standards, usually supplemented by third-party potency, microbiological, and heavy-metal testing plus a certificate of analysis for each batch.
Can gummy production scale from small pilot runs to full commercial production?
Yes. A manufacturer with flexible MOQs, pilot equipment that mimics commercial cooking and depositing, and scalable drying capacity can move a formulation from the pilot stage to full commercial production while keeping the product consistent.
This article is provided by Gothink Biology, a globally recognized dietary supplement manufacturer.
Shenzhen Gothink Biotechnology Co., Ltd. is a leading global nutritional supplement supplier and dietary supplement manufacturer, specializing in OEM, ODM, CMO, and CDMO services for health and wellness brands worldwide. With extensive industry experience and multiple international certifications—including ISO 9001, ISO 22000, HACCP, FDA, HALAL, GMP, KOSHER, BRC, FSSC 22000, PJPH, and Vegan—we provide B2B clients across global markets with high-quality custom formulations, contract manufacturing, and wholesale solutions.
For more information, please visit our official website at https://gttbio.com/ or contact our expert team.